This article is a transcript from a podcast by Siemens.
My name is Ian Walls and I’m an engineer. I finished episode 1 of this 4-part series on Smart Manufacturing by mentioning the evolving role of the Manufacturing Engineer in Smart Manufacturing deployments and that’s something I’ll explore further in this episode.
The Manufacturing Engineer’s core mission: bridging design to production
I like simple definitions. Engineers, myself included, typically think about the flow of information between engineering and manufacturing as a left-to-right flow, from design to production. The role of a Manufacturing Engineer is to get you from the left-hand side of my mental picture over to the right.
On the left we’ve got a design, effectively a product that’s waiting to be built. And on the right is a factory floor that’s waiting to receive a work instruction build it. The role of the Manufacturing Engineer is to enable this.
This involves first of all taking a manufacturing view of the Bill of Materials (BOM).
In the manufacturing world, we want to take a view of the BOM that typically reflects the build sequence. This is how we’re going to put it together. We recast the design BOM information in a way that makes sense in a manufacturing context, creating a Manufacturing BOM, or MBOM. That might mean also including non-modelled parts, such as grease or thread. Then we take this MBOM and incorporate it into a process definition, known as the Bill of Process. It’s analogous to a BOM, but describes the operations that you go through to make a product. Thus it references parts from the manufacturing BOM, it references a location within your facilities where you’re going to make it such as a station on a build line, and it references resources such as tooling and jigs that are required to build the product. This Bill of Process is the key output from the Manufacturing Engineer. It becomes the context in which you can author work instructions, for example, or information about the timing and frequency of various manufacturing operations, helping you balance an assembly line. These are the role-specific tasks for which a Manufacturing Engineer is responsible.
But the role of the Manufacturing Engineer is not only to author a set of work instructions or define a process, but to validate them. And because what we’re talking about is doing this as much as possible in the digital world, that validation is simulation, and different types of simulation are needed to validate different aspects of that manufacturing process.
The third key strand relates to quality and Manufacturing Engineers have a key role in defining the product quality or at least the manufacturing process quality. That is, how the process is executed on the shop floor. Through things like control and inspection plans that we can perhaps look at in more detail in a later episode.
These then are the essentials of the Manufacturing Engineer role. The role has been around for as long as manufacturing has, but increasingly, involves performing these tasks virtually rather than in the real world.
This drives value in two ways for a business. Firstly, because you can do things digitally earlier than the alternative – building a prototype on the actual line, proving out the process, iterating on the original prototype – you can compress the overall lead time to get a product into market. It shortens the new product introduction cycle.
The value proposition: unlocking efficiency with concurrent engineering
But I think more important than that is the recognition that by doing things earlier, you can start doing them in parallel with the design activities. This is known as concurrent engineering. The concept has been around for decades, but it’s still really uncommon to see it implemented in practice in British industry. It offers tremendous possibilities, because if you’re doing the manufacturing definition at an early enough stage, the Manufacturing Engineer can actually influence the product design. Influence it to make it easier to assemble, easier to test, easier to disassemble and maintain in the field. We talk about this as being designed for manufacture, design for assembly, designed for test. Sometimes it’s abbreviated to DFX and it enables an engineer to identify problems with the process before it exists in the physical world. Since it costs little to make changes and iterate in the digital world, this becomes a key way in which digital manufacturing delivers value to an organization.
ERP vs PLM?
Now let’s think about the systems required to enable us to pull activities forward and do things earlier. My customers often tell me this can be done in ERP and there is no need for specialized software such as a PLM system.
I certainly don’t see a conflict between ERP and PLM systems. The BOMs and routings defined in the PLM system are required by in the ERP system. What I would very clearly say is that product and process definitions should be done in the PLM environment, because there you’re doing it close to the design activity. Which brings me back to the point I made earlier about concurrent engineering and performing tasks in parallel. You can perform these engineering tasks much more effectively in a system or environment where you have access to that rich set of engineering data, such as 3D designs of the product, 3D information about the facility, the tooling and jigs and fixtures and much more. And then at the at the appropriate point, move that definition across to the ERP system. So I don’t see that there’s a fundamental conflict. I think it’s just a question of where you do the authoring of this information.
Pulling engineering tasks forward, doing them earlier in PLM rather than waiting and doing them later in ERP yields many benefits. I’ve seen this multiple times across many industries. I recently worked with a heavy equipment manufacturer and a firm believer in doing things the traditional way, with physical prototypes, physical testing and real-time adaptation of processes to address issues on the production floor. We worked with them to construct a digital twin of that build process. We brought the stakeholders into a room and together we stepped through the build process in that virtual environment. The geometry of the product involved was quite complex and so it was difficult to visualize out in the production hall how the parts would come together. But that’s not an issue when you work in-silico. By working through the process virtually they identified a problem with tooling that, had it been discovered after build had started rather than before would have cost in excess of £100,000 to fix. And that was just a recent engagement. I’ve seen similar things many times in the past.
Empowering the Manufacturing Engineer: the right tools for the job
Now that we’re thinking about systems, and I hope I’m not rambling too much here, I’d like to bring the discussion back to the role of the Manufacturing Engineer. When I ask Engineering Managers what proportion of time their people spend on different tasks, authoring work instructions is typically at the top of the list of things that consume their time. It’s not at all unusual to see Manufacturing Engineers spend half their time authoring and maintaining work instructions, often using tools like PowerPoint or Word.
It is hugely inefficient to do this with office productivity tools. Creating a work instruction might involve a screenshot from a CAD workstation, some information that has to be typed in, you might go to the line and take some photographs and embed them as jpegs. This is not what office productivity tools are designed for. And the assets that are being created are not persistent. So when change occurs, as it invariably does, the Manufacturing Engineer has to loop back and update everything.
With its direct links to engineering data, preconfigured work instruction templates and rich visual content, Teamcenter PLM is the ideal environment for authoring and maintaining work instructions.
Much of the data needed for a work instruction is immediately accessible, almost as a byproduct of having created the Bill of Process. Because you know which parts are impacted, you know the tooling involved, where in the line it’s being assembled and you’ve got the 3D geometry that you can embed in that work instruction. And the beauty is that it’s all persistent. And it is managed and maintained in the PLM system. So when change happens, there’s a workflow to support it. The information comes to the Manufacturing Engineer who can make whatever changes are needed, press the return key and that’s it.
Taking simulation to the next level
Reusing the 3D information in work instructions is increasingly common, as is product development and even factory definitions in 3D. But when I think about 3D, I think about simulation. Because if we can make a 3D model actually behave as it’s going to behave in real life, that provides us with a completely different frame of reference for the model.
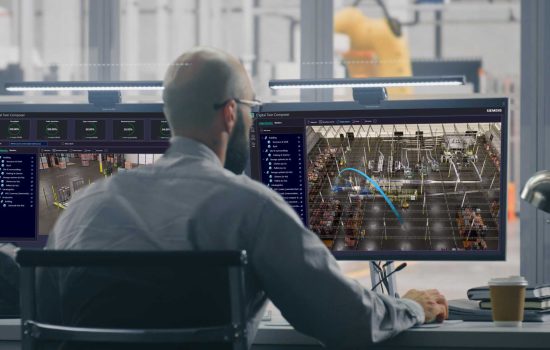
For over 30 years I’ve been building simulations and advocating that my customers do that too. There are some very fixed opinions out there about the cost of simulations and the value that they deliver. The challenge is that although it’s now a very mature technology, companies haven’t really embedded it into their processes. It’s usually seen as a sort of side venture with no commitment to using it as part of an end-to-end process. That possibly reflects simulation as it was 20 years ago, very much a standalone tool that required specialist skills to manage and manipulate the data. But all of that has changed. The user interfaces and interactions are far more intuitive and there’s much higher levels of out-of-the-box functionality than previously. And increasingly, we see these tools embedded in this overall workflow around the PLM process. So the data that we’re talking about – the 3D data and the process data – is immediately accessible by these simulation tools, significantly reducing the amount of effort required to build these simulations.
And that means the simulations are more persistent. They can adapt as the process itself adapts. So, you’re not developing these one-shot models that were correct on the day you validated them and got some value from, but thereafter become too difficult to maintain. If you can take that away and keep those models up-to-date then you can continue extracting value. And if we connect this tool to assets in the factory then simulation – once seen as a strategic tool – becomes an operational tool. We can take a live feed of information from the shop floor and feed that into the simulation. The model has been updated with real data and can be used as a decision support tool on a day-to-day basis. In my opinion, this greatly expands the value of simulation.
The future is now: AI’s impact on Smart Manufacturing
Now let’s think about the implications of AI for Smart Manufacturing. I can understand why people feel it’s hype. I mean, we’re bombarded with it from all directions. We are right to question things – it helps define us as engineers – and to see beyond the marketing.
But having said that, I am convinced that AI will revolutionize the way that many jobs are performed and the Manufacturing Engineer’s role will be exception. Siemens is investing heavily, with more than 1400 engineers dedicated to AI. We’re starting to see this come through in the products themselves. We see the Copilot type application, which is about simplifying the user interaction and enabling natural language interactions with the models. So that you can tell it that you want to achieve this or that. The AI will interpret that and translate that into the correct menu options and in doing so, change and improve the user experience. Beyond that I’m very excited about the possibilities it offers for interacting with large swaths of legacy data. You might use it to extract information from work instructions that exist in multiple formats and structures. The application of AI on the factory floor is limited only by our own imaginations and this is something we might return to in a future episode.
Rethinking quality management in Smart Manufacturing
I’ll finish up with some thoughts on quality management in the Smart Manufacturing context. In terms of organizational structure quality management is often owned by the Quality Department. But the touch points that define product quality all live in the engineering and manufacturing execution domains, and it doesn’t really make any sense to me that this is somehow seen as a separate silo. We have a manufacturing process, and the Manufacturing Engineer needs to determine the risks associated with executing that process. The classic tool for doing that is Failure Mode and Effects Analysis and process Failure Mode and Effects Analysis in particular. Commonly, this is done as a retrospective exercise, enabling us to tick the quality box on our checklist. But we don’t get value from it because we usually cannot use the outputs to change the way that we do things.
In a concurrent engineering environment, the manufacturing process is defined in parallel with the product engineering process. If we do the quality risk assessment at that stage as well, we use the results to inform both processes. By making the changes at source we’ll see higher quality processes right from the outset. And then the step beyond that is to say that we’ve assessed this risk, there’s still some residual risks that we need to mitigate on the shop floor and then we put in place a control and inspection plan. But that’s a topic we can perhaps devote more time to in a future episode.
If you’d rather listen to my thoughts than read, check out my Podcast. In the meantime, if you wish to reach out to me and have a conversation about any of the topics I’ve discussed and how it might apply in your manufacturing context, I’d be delighted to speak to you. I can be reached by e-mail at [email protected]. I will leave you with a quote from the investor Peter Drucker ‘The best way to predict the future is to create it’.
Until the next time, goodbye.
Ian Walls, Portfolio Development Executive, Digital Manufacturing, Siemens Digital Industries Software.
Ian’s primary focus is the software portfolio supporting Digital Manufacturing. This encompasses manufacturing process planning; plant design, simulation and optimization; Part Manufacturing and CAM; and Additive Manufacturing; production scheduling; Manufacturing Execution; and Quality.
Ian has been with Siemens for over 30 years. In that time, he has been involved in sales; presales; services delivery; training; and support; for customers spanning a broad range of industries both in the UK and around the world.
For more articles like this, visit our Digital Transformation channel/